Expert Wear Plate Processing
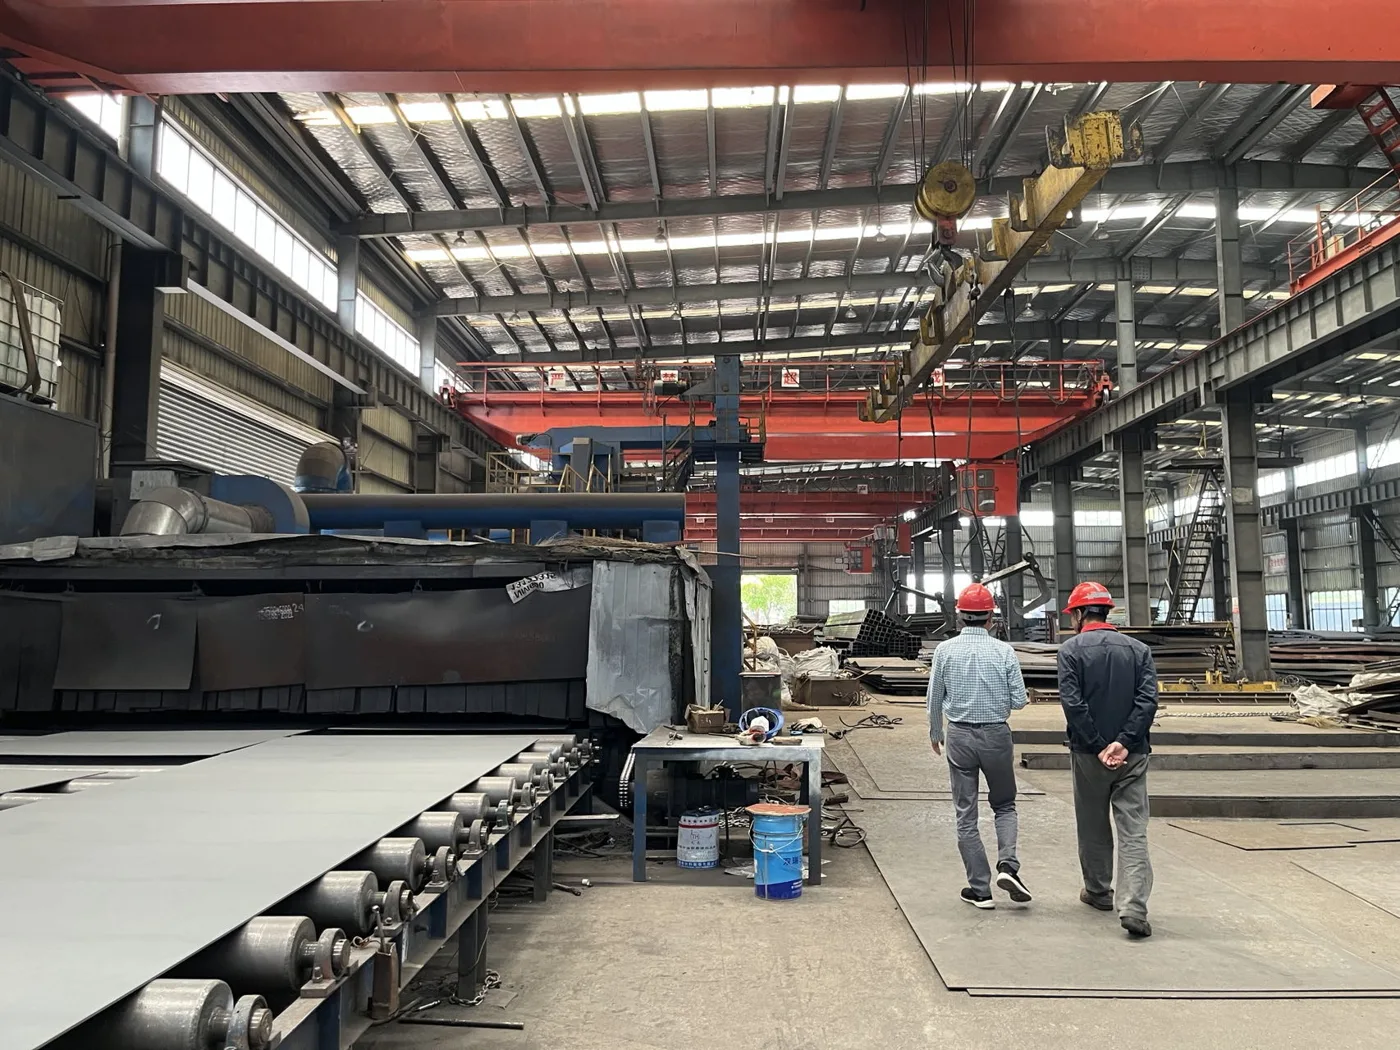
Advanced Machines and Processing Methods
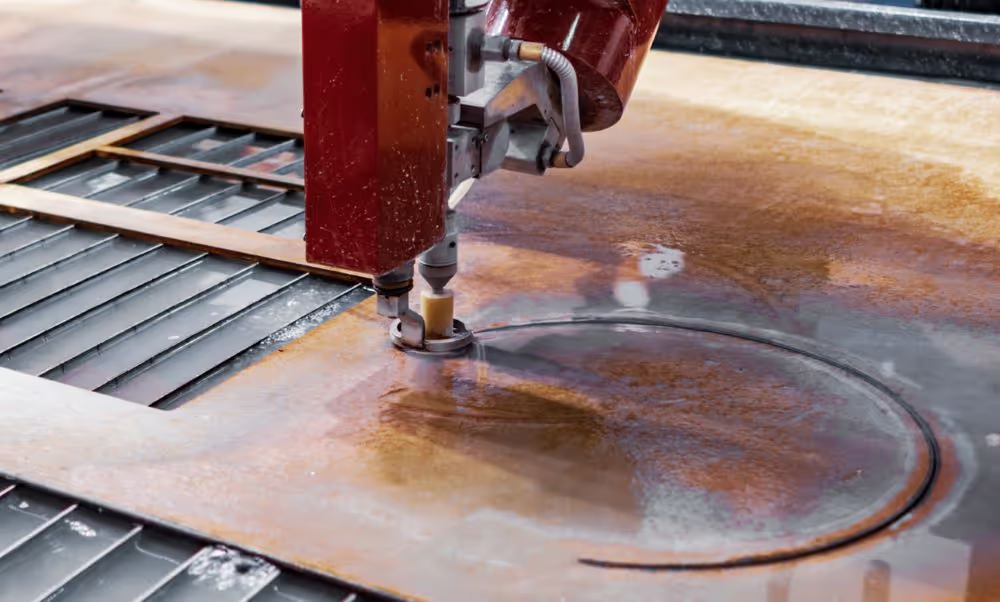
Laser Cutting
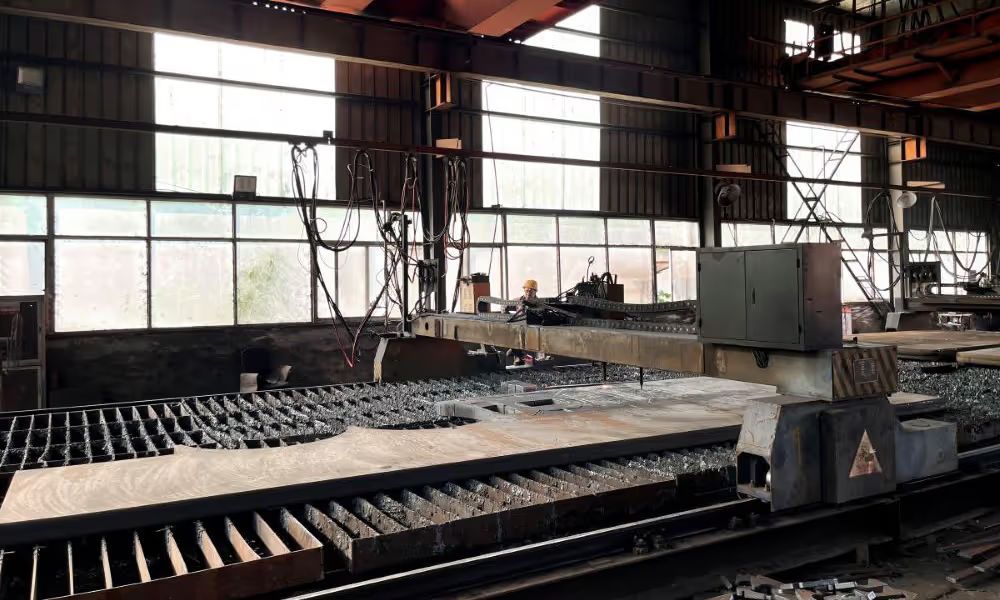
Our workshop operates several 60 kW high-power laser cutting machines, cutting wear plate and high-strength plate to your drawings — from single parts to full batches. Send your DXF/DWG and we quote cutting together with the plate price.
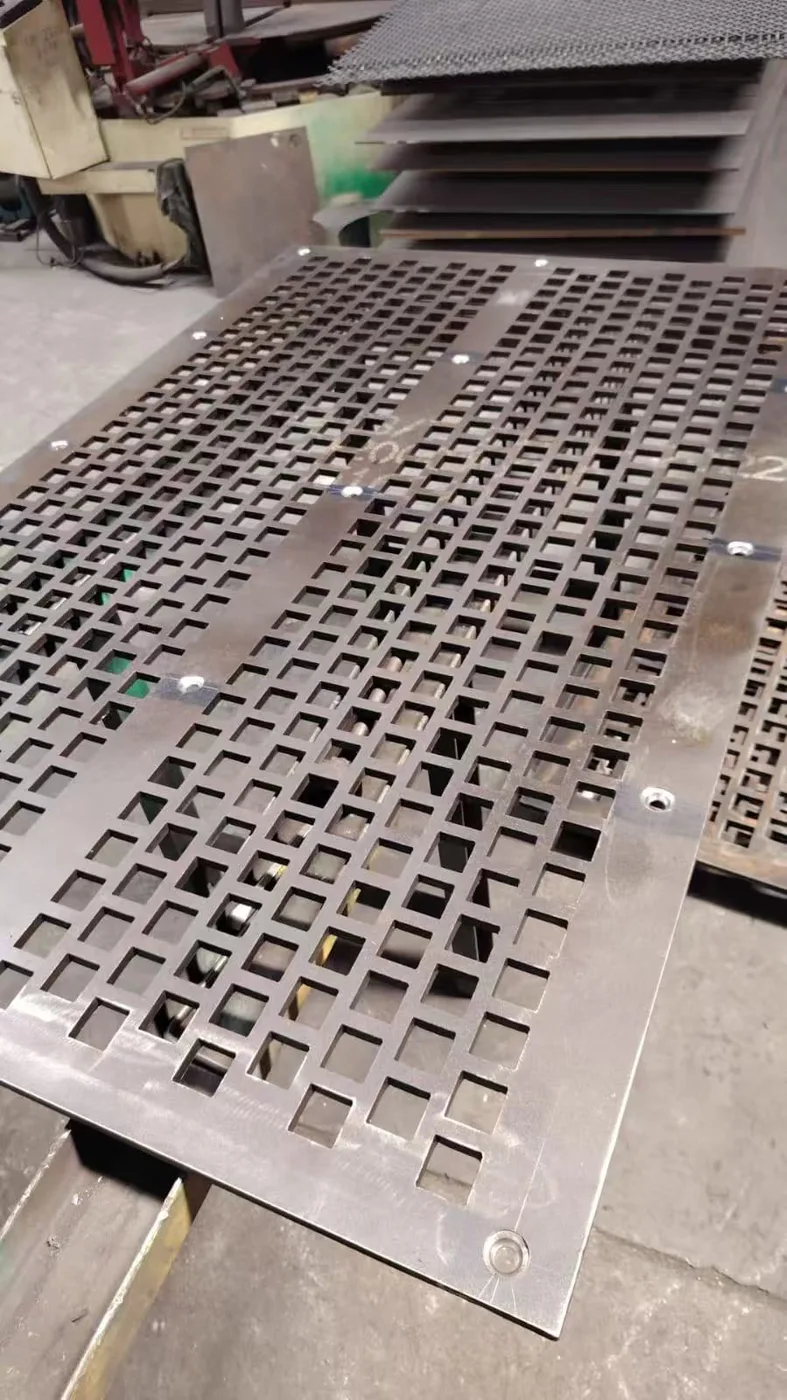
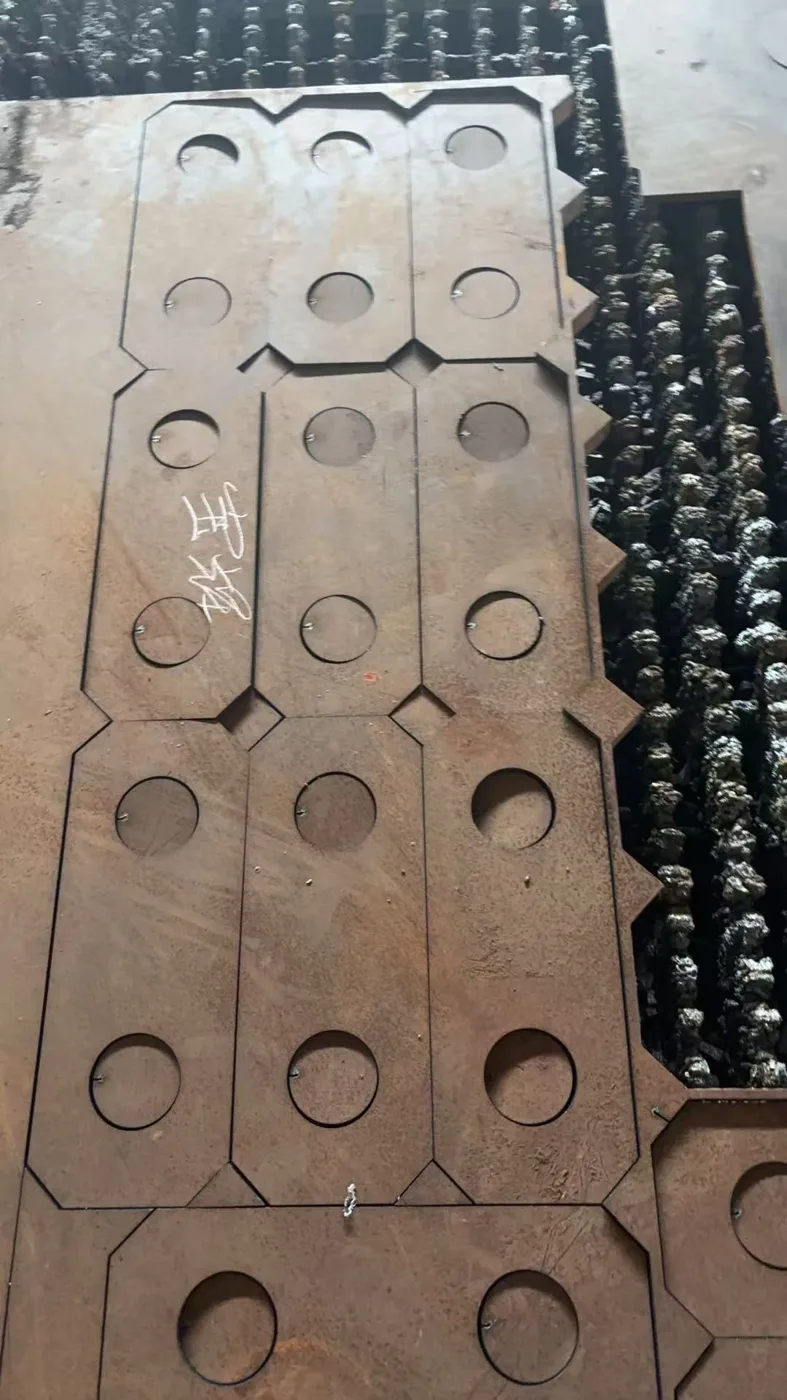
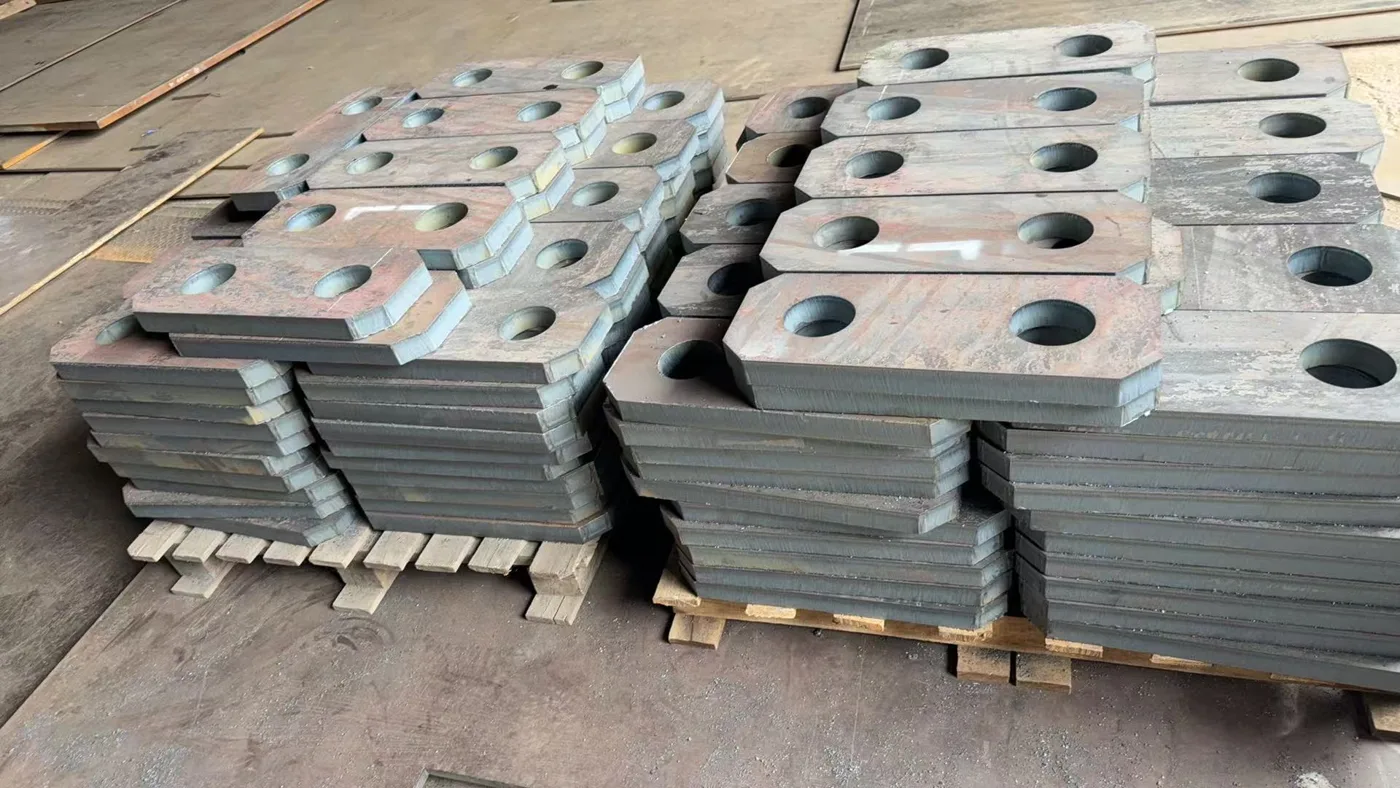
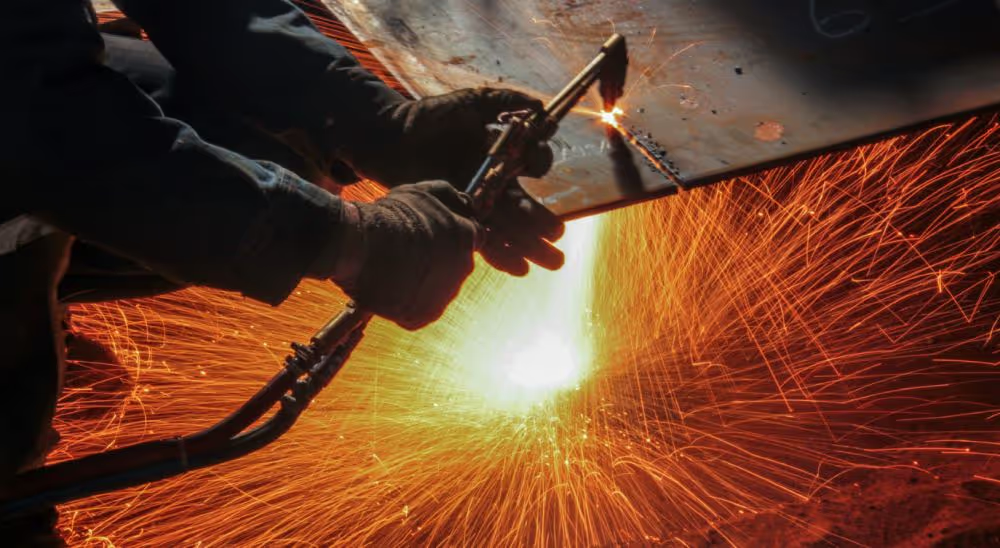
Thermal Cutting
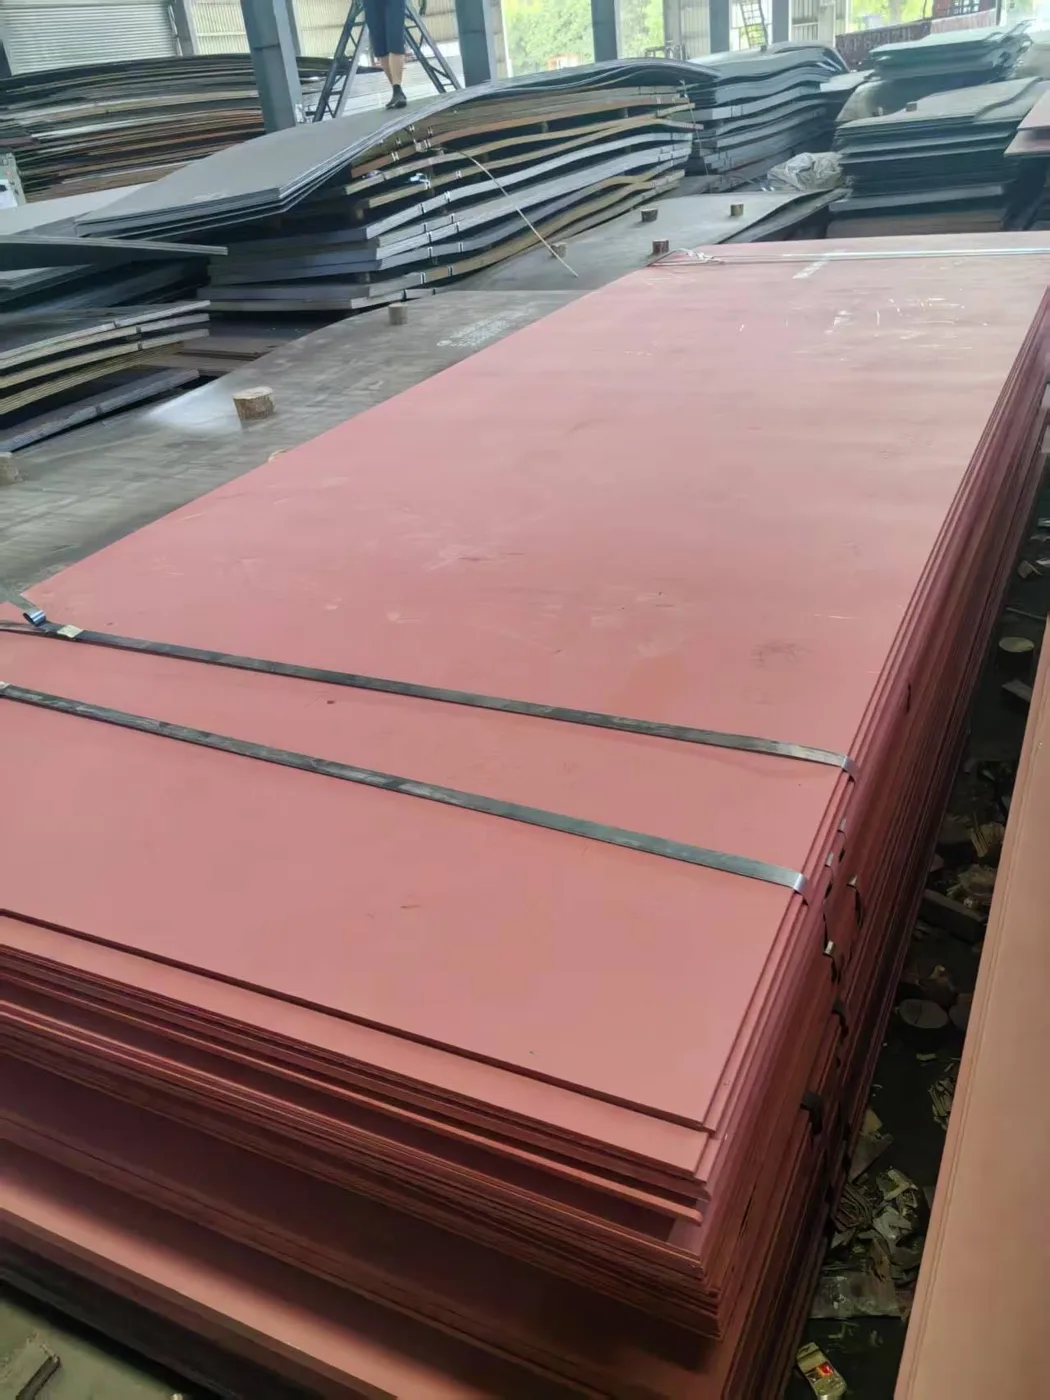
Shot Blasting & Primer Painting
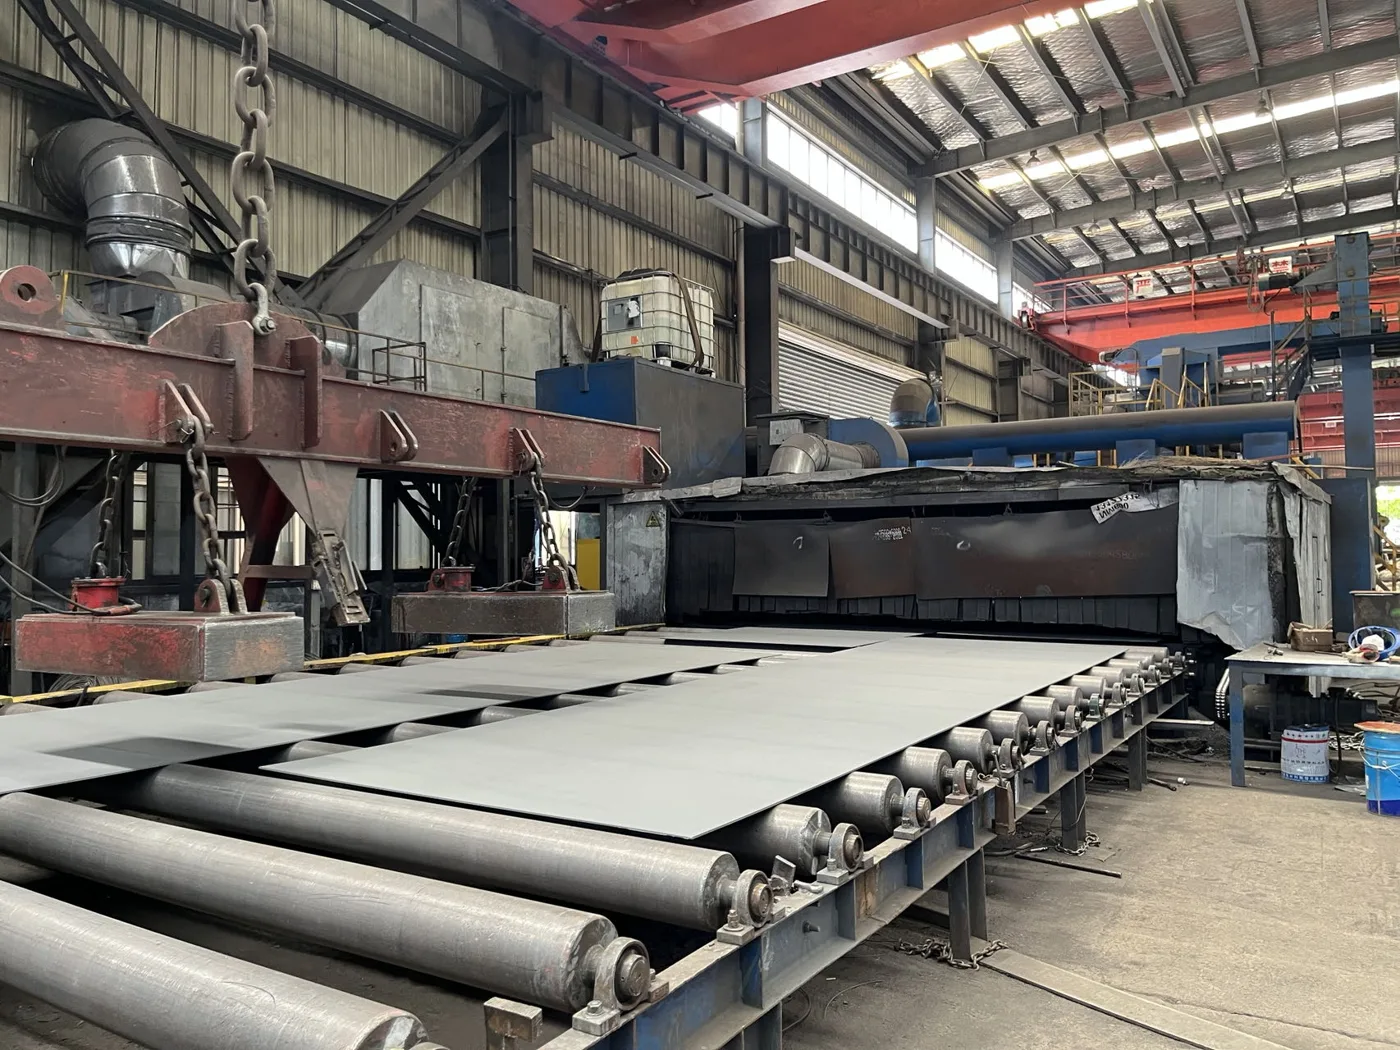
Every plate can leave our workshop fully surface-treated. Plates pass through an automatic shot-blasting line to SA 2.5 (near-white metal), then receive a coat of premium-brand anti-rust primer.
- Blasting grade: SA 2.5 per ISO 8501-1
- Dry film thickness: 15–50 μm, tuned to your climate and transit time
- Colors: red and grey as standard — any RAL color on request
- Stenciling: grade, heat number and your markings, printed to your specification
- Purpose: stops flash rust between production and installation — essential for sea freight in humid seasons
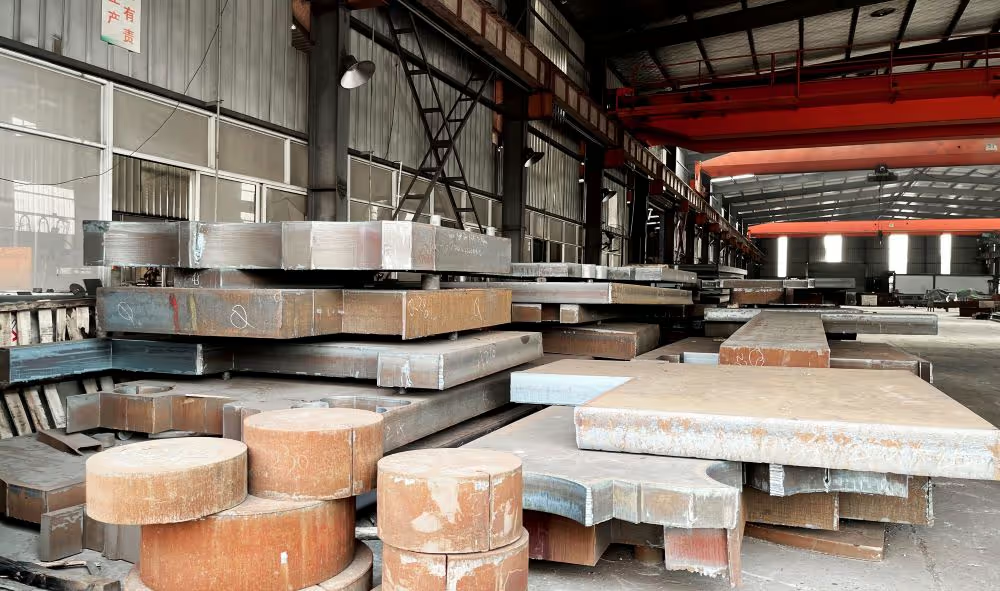
Wear-resistant plates, or abrasion-resistant plates, are crucial in industries where durability against wear and tear is paramount. These plates are valued for their high alloy content and hardness, but improper processing can lead to cracking. Here, we discuss common types of cracking and effective strategies to mitigate them.
Common Types of Cracking During Processing
Cut-Edge Cracking
Occurs with thermal cutting methods (flame, plasma, laser) and is visible from 48 hours up to several weeks post-cutting. Influenced by hydrogen content and residual stresses in the steel plate.Definition & Causes:
Prevention Tips:
- Initiate cutting while the material is still warm to reduce the risk.Pre-Heat the Plate:
- This reduces residual stress, though not as effectively as pre-heating.Slow Cutting Speed:
- Apply heat immediately after cutting and allow slow cooling to minimize cracking risk.Post-Heat or Slow Cooling:
Weld Cracking
Challenging due to cracking in the weld metal or heat-affected zone, influenced by cooling speed, hydrogen content, and filler metal.Definition & Causes:
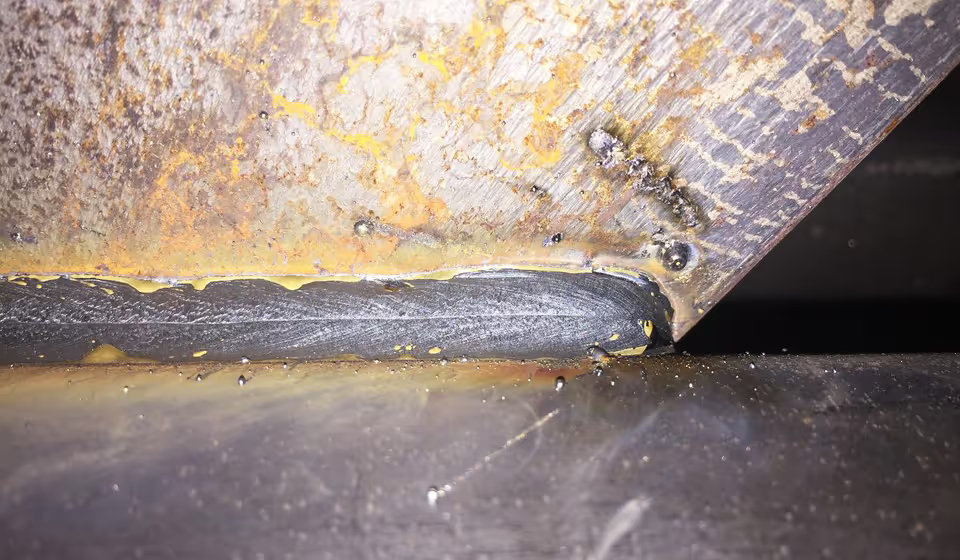
Prevention Tips:
- Ensure joint cleanliness to prevent hydrogen cracking.Clean Welding Surface:
- Similar to cutting, these methods reduce the heat-affected zone and prevent cracking.Pre-Heating & Slow Cooling:
- Choose filler metal based on the base metal’s tensile strength to combat cracking.Appropriate Filler Metal:
Bend Cracking
Difficult due to the plate’s high strength and poor elasticity.Definition & Causes:
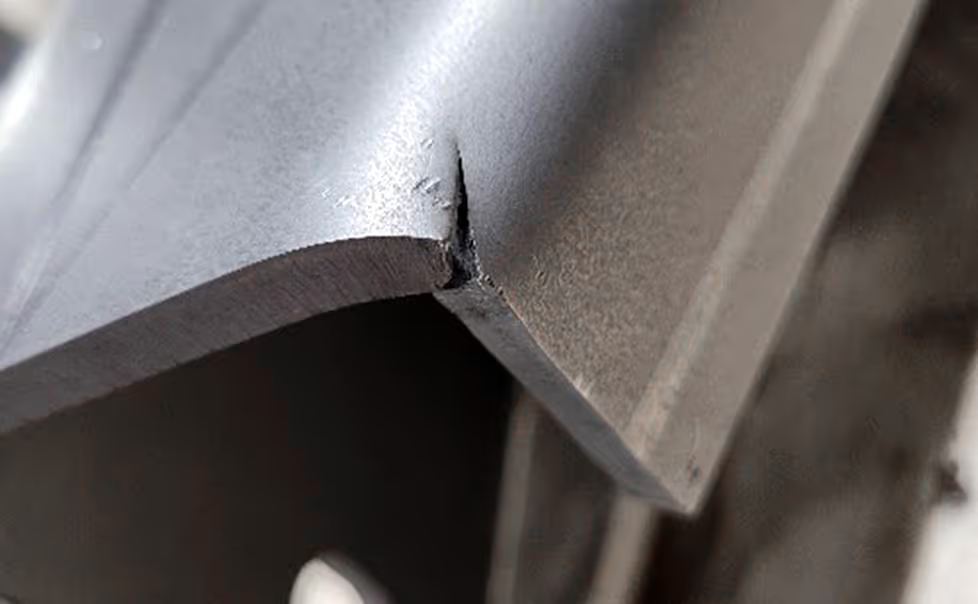
Prevention Tips:
- Before bending, understand the allowable bending degree on the product quality certificateCheck Inspection Certificate:
- Ensure precise bending to achieve flawless finished products.Account for Bend Allowance:
- Guarantees a smooth, clean productUse a Press Brake:
Steel Plates Purchased Through Official Channels from Baohui Steel Limited Come with an Inspection Certificate as Shown Below
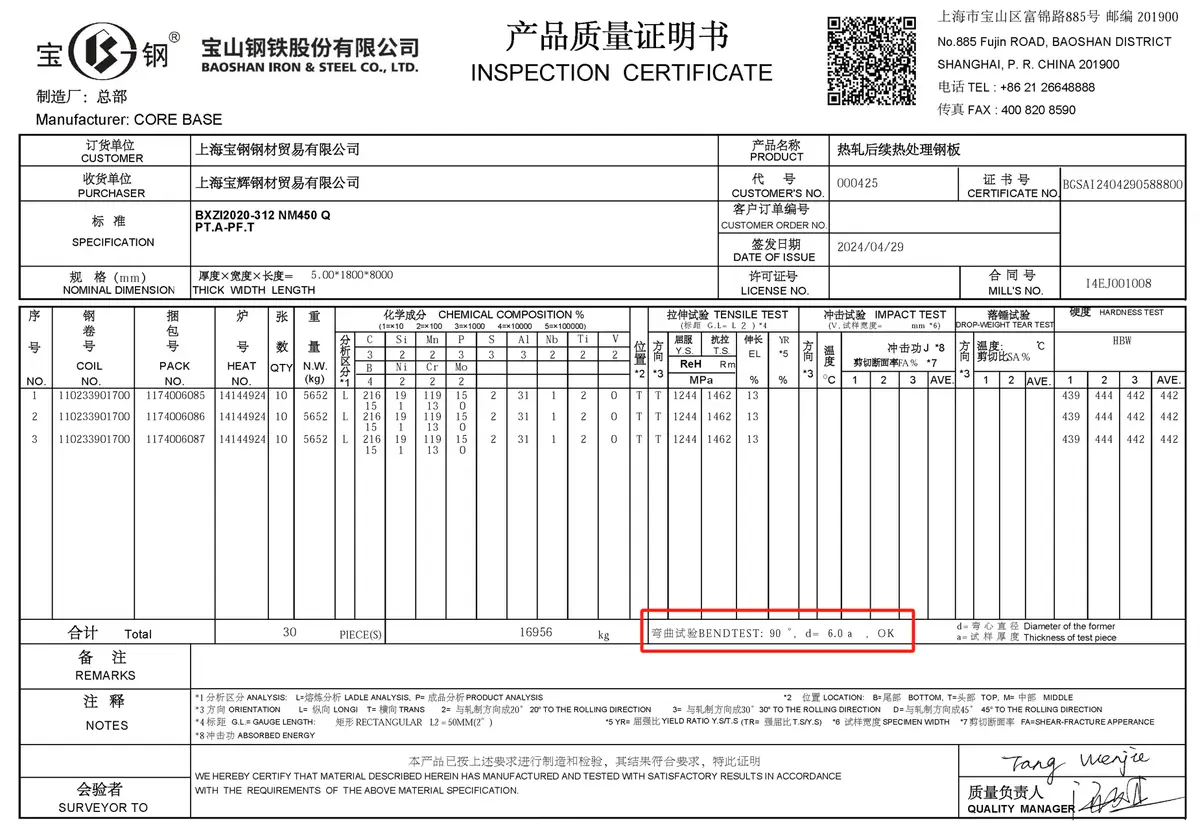
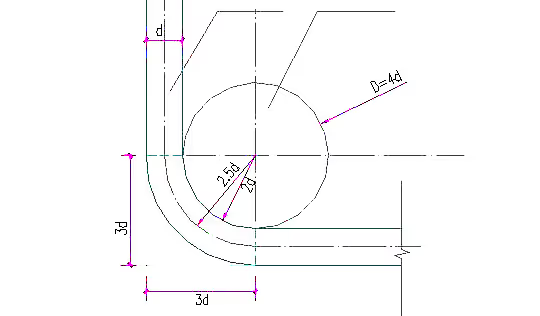
In the product quality certificate, you can find a section labeled "Bend Test," which specifies the safety margins to be observed during bending.
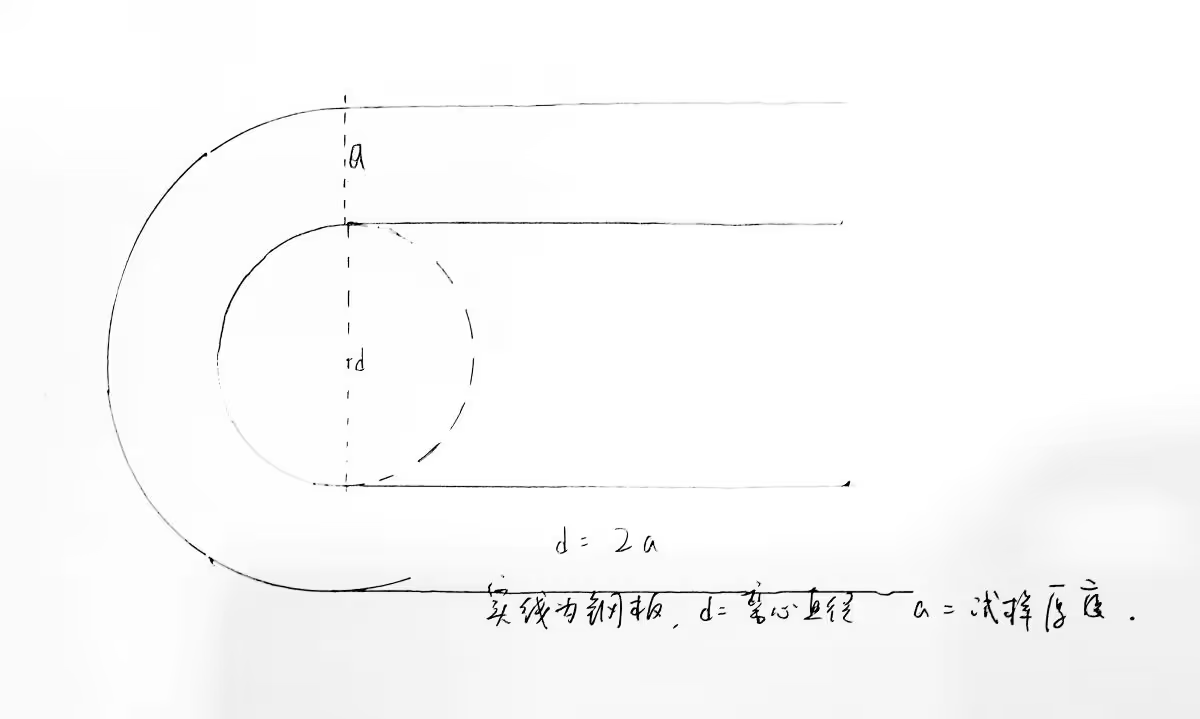
- The "90°" represents the maximum bending angle.
- "D" represents the minimum diameter of the bending center.
- "A" represents the thickness of the steel plate.
For businesses utilizing wear-resistant steels, high-strength steels, or other thick steel materials, implementing proper measures to prevent cracking can significantly reduce costs. Always consult the processing guide specific to your plate brand, as each mill has its own standards for pre-heat temperature, cutting speed, and filler metal. Adhering to these guidelines can largely prevent cracking issues.Suggestion:
, with a decade of experience led by an internationally renowned team, specializes in trading wear-resistant steel plates. Our sales engineers, technicians, and consultants are ready to assist you in selecting the most suitable steel and employing the most efficient manufacturing processes. For a tailored supply solution, contact us at .Baohui Steel Limited[email protected]
Processing FAQ
Can you cut wear plate and high-strength plate to size?
Yes — flame, plasma and laser cutting to your drawings. Send them at the quotation stage and we include cutting in the same FOB price.
What blasting grade and paint do you use?
Automatic shot blasting to SA 2.5 (ISO 8501-1), followed by premium-brand anti-rust primer at 15–50 μm dry film thickness, depending on your climate and transit time.
Can the paint color and stenciling be customized?
Standard colors are red and grey; any RAL color is available on request. We stencil grade, heat number and your own markings to your specification.
Does cutting or blasting affect the plate certificate?
No. The mill test certificate stays with the original heat; we record the heat numbers of every plate we process so traceability is preserved.
How long does processing add to the lead time?
Typically 3–7 working days for cutting, blasting and painting together, depending on quantity — much faster than booking these services separately at destination.